Support the flexible strip and locate its slots with cameras.
06
Tension & insert
Use controlled restraint and monitor insertion / seating.
07
Inspect the core
Check each placement, then the finished grid and height.
08
Apply adhesive
Use the selected drip or spray recipe after acceptance.
DRIP RECIPE
Meter adhesive at strip intersections. Covers remain retracted.
OR
SPRAY RECIPE
Deploy fixture covers and confirm extraction before spraying.
AMBIENT CURE & OUTPUT
Support the core during the agreed hold period. Operator assists unloading.
Both adhesive modes are included in the complete assembly quotation. They are alternative recipes, not two mandatory consecutive operations. Failed or uncertain inspection results trigger a controlled hold and recovery.
02 / FOUR QUOTATIONS
Separate scopes. Clear development decisions.
The POCs establish feasibility before production procurement. Each workstream can be ordered separately.
New cutting station through automatic assembly-loading transfer
32–40 weeks, including POC
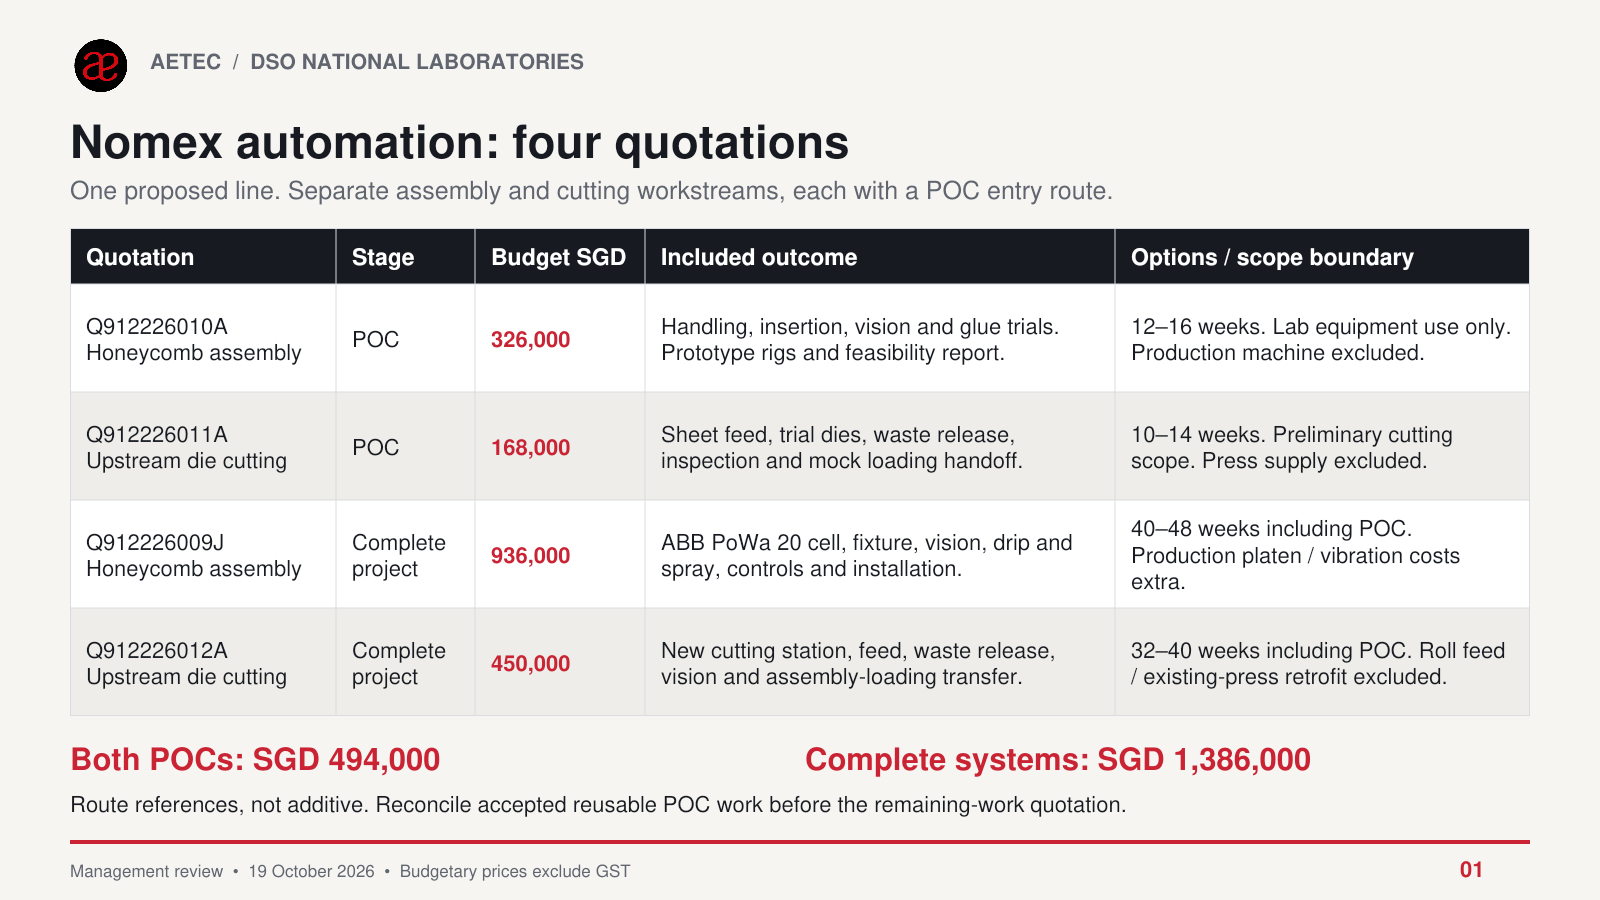
Both POCsSGD 494,000
Both complete-project budgetsSGD 1,386,000
All prices exclude GST. These are separate route references, not additive totals. Schedules start after the required order, payment, approved inputs and sample availability.
01 / ASSEMBLY POCSGD 326,000
Flexible-paper process validation
Q912226010A
Supported vacuum / jaw gripper and spring-tension fixture prototypes.
Short-strip, 5 × 5-cell and sparse full-width insertion trials.
Camera alignment, inspection, drip and spray testing.
POC-scale platen / vibration comparison and a moving cover segment.
Defined campaign
300 pickup attempts, 30 full-width insertions and up to 3 combined gripper / fixture refinement cycles.
Deliverable and boundary
Prototype records, final feasibility report and production recommendation. Production robot, complete machine and site SAT are excluded.
02 / CUTTING POCSGD 168,000
Cutting, release and strip handoff
Q912226011A
Sheet separation, registration and visible cut-quality assessment.
One coupon die and one nominal full-width trial die.
Waste separation and supported transfer to a mock loading datum.
Trial controls, fault recovery and interface definition.
Defined campaign
180 coupon strokes, 30 full-width cutting attempts, 60 transfers and up to 2 combined refinements.
Deliverable and boundary
Trial tooling records, feasibility report and production recommendation. General-purpose trial press supply and production line integration are excluded.
03 / COMPLETE ASSEMBLYSGD 936,000
Robotic honeycomb assembly cell
Q912226009J / Revision J
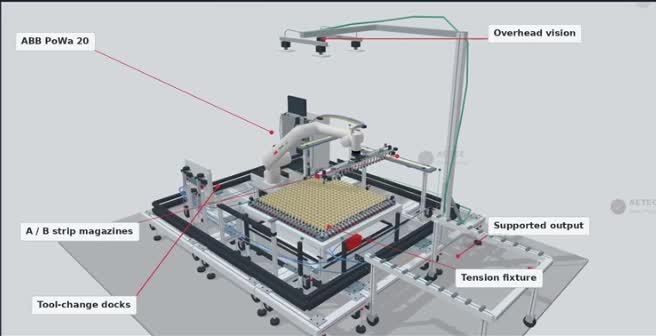
ABB PoWa 20, supported handling, tension fixture and modular frame.
Alignment cameras, post-placement inspection, core and height checks.
Drip and spray heads, separate circuits and automatic spray covers.
Controls, local PC interface, drawings, FAT, Singapore installation, SAT and training.
Production platen / vibration requires separate pricing. Upstream cutting and transfer are outside this assembly quote. Manual replenishment and supported unloading remain the base.
04 / COMPLETE CUTTINGSGD 450,000
Automated sheet-to-strip system
Q912226012A
New guarded cutting station, sheet magazine and registered feed.
Production tooling, supported release and waste collection.
Vision, A/B strip buffer, loading transfer and controller handshakes.
Controls, safeguards, engineering records, FAT, Singapore installation, SAT and training.
Budget allocation
Equipment / tooling 348k. Development / design / software 65k. Integration and handover 37k.
Options and exclusions
Assembly machine is separate. Roll feed, extra formats and existing-press retrofit require separate assessment and pricing. Manual stock replenishment and bin emptying remain the base.
Common basis: one agreed Nomex grade / thickness and A/B family, with defined trial quantities. Cutting uses one sheet format. The upstream concept remains preliminary pending approved sheet and strip drawings, press suitability and trials. Unlisted work requires a separately approved scope and price.
03 / DEVELOPMENT ROUTE
POC first, then a production decision
Management can proceed, revise the scope or stop after reviewing the measured results and remaining risks.
ASSEMBLYQ912226010A POC trials
FEASIBILITY REVIEWResults, risks and updated remaining scope / price
ASSEMBLYQ912226009J Complete-project reference
CUTTINGQ912226011A POC trials
FEASIBILITY REVIEWCut quality, waste release and loading interface
CUTTINGQ912226012A Complete-project reference
AETEC proposes this phased approach. POC success supports the next design stage but does not certify production takt, yield or bond strength. Production procurement follows the relevant approvals. Shared interface work will be reconciled if both POCs are ordered.
04 / PROJECT FILM
The proposed system in operation
The supplied 9-minute reference video explains the intended layout, robot handling, inspection, glue application and upstream interface.
Video ready. Press play to start.
Download preserves the supplied video and audio. Allow time to prepare the full file.
Engineering concept animation. It illustrates the intended sequence and does not constitute production-performance validation or a manufacturing release.
05 / MANAGEMENT PRESENTATION
Five slides for the decision meeting
One consolidated comparison followed by one slide for each quotation. Includes scope, budget, key boundaries and reference visuals.